O1 Steel
The classic oil-hardening tool-grade steel, alloyed with manganese-chromium-tungsten. Very good machinability, high hardness after quenching, and low cost. For small tools and low-volume dies. It is oil quenched at relatively low temperatures with low distortion, reaching up to 65 HRC; its good machinability in the annealed condition makes complex machining easier before hardening.
| SAE / AISI | EN | DIN | JIS |
|---|---|---|---|
| O1 | 100MnCrW4 | 1.2510 | ≈ SKS3 |
| % | C | Si | Mn | Cr | W | V | P | S |
|---|---|---|---|---|---|---|---|---|
| Min | 0.85 | 0.10 | 1.00 | 0.40 | 0.40 | — | — | — |
| Max | 1.00 | 0.50 | 1.40 | 0.70 | 0.60 | 0.30 | 0.030 | 0.030 |
 Hot forgedAnnealed
 Hot rolledAnnealed
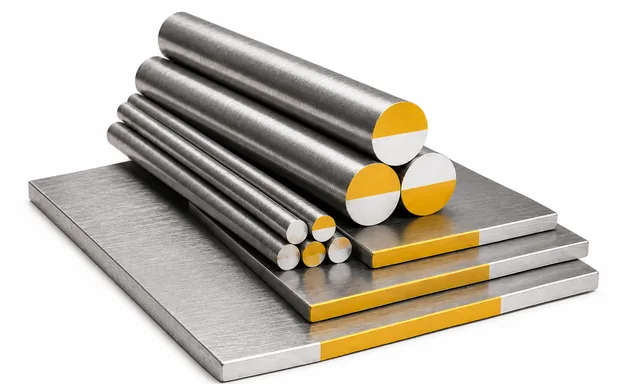
 Plates1/8" – 12"3 mm – 305 mm
 Round bars1/8" – 2"3 mm – 51 mm
- Cutting dies
- Precision punches
- Forming dies
- Industrial knives
- Precision gages
- Master gages
- Threading taps
- Reamers
- Cutting broaches
Note: The information and values in this data sheet are provided for reference only and may vary depending on manufacturing, treatment and application conditions. They do not constitute guaranteed specifications, so use and interpretation of this data is the user's responsibility.
Total or partial reproduction of this document is prohibited without prior authorization.